Pipeline Detection Equipment Transport Case — Reliable Transport Solutions for Smart Detection Devices
5 Key Takeaways: Pipeline Detection Equipment Transport Case — Reliable Trans
- Topic: Pipeline — industry context for B2B buyers and procurement teams
- Date: 2026-09-11 — current standards, certifications and market conditions
- Applications: protective cases for industrial tools, MRO, photography, drones, defense, medical devices, marine, audio
- Procurement: MOQ 500 pieces per Pantone color, 30–45 days lead time after tooling approval, CE/RoHS/REACH/ISO 9001
- Shipping: EXW Guangdong (pickup) or FOB Shenzhen / Ningbo (sea freight). 28–35 days to Hamburg / Rotterdam
5 Key Takeaways
- Full Protection: Waterproof, shockproof, anti-static, and corrosion-resistant — engineered for complex field environments
- Lightweight & Portable: Precision-engineered for ease of transport and field deployment
- Customizable Interior: Adjustable dividers adapt to any pipeline detection equipment configuration
- Professional Appearance: Custom logo and color options for brand consistency
- Proven Across Applications: Trusted by CCTV robots, sonar detectors, ultrasonic detectors, and magnetic flux detectors
Table of Contents
- What Is a Pipeline Detection Equipment Transport Case?
- Core Protective Features
- Applicable Equipment Types
- Why Choose KeXinMaterials
- FAQ
1. What Is a Pipeline Detection Equipment Transport Case?
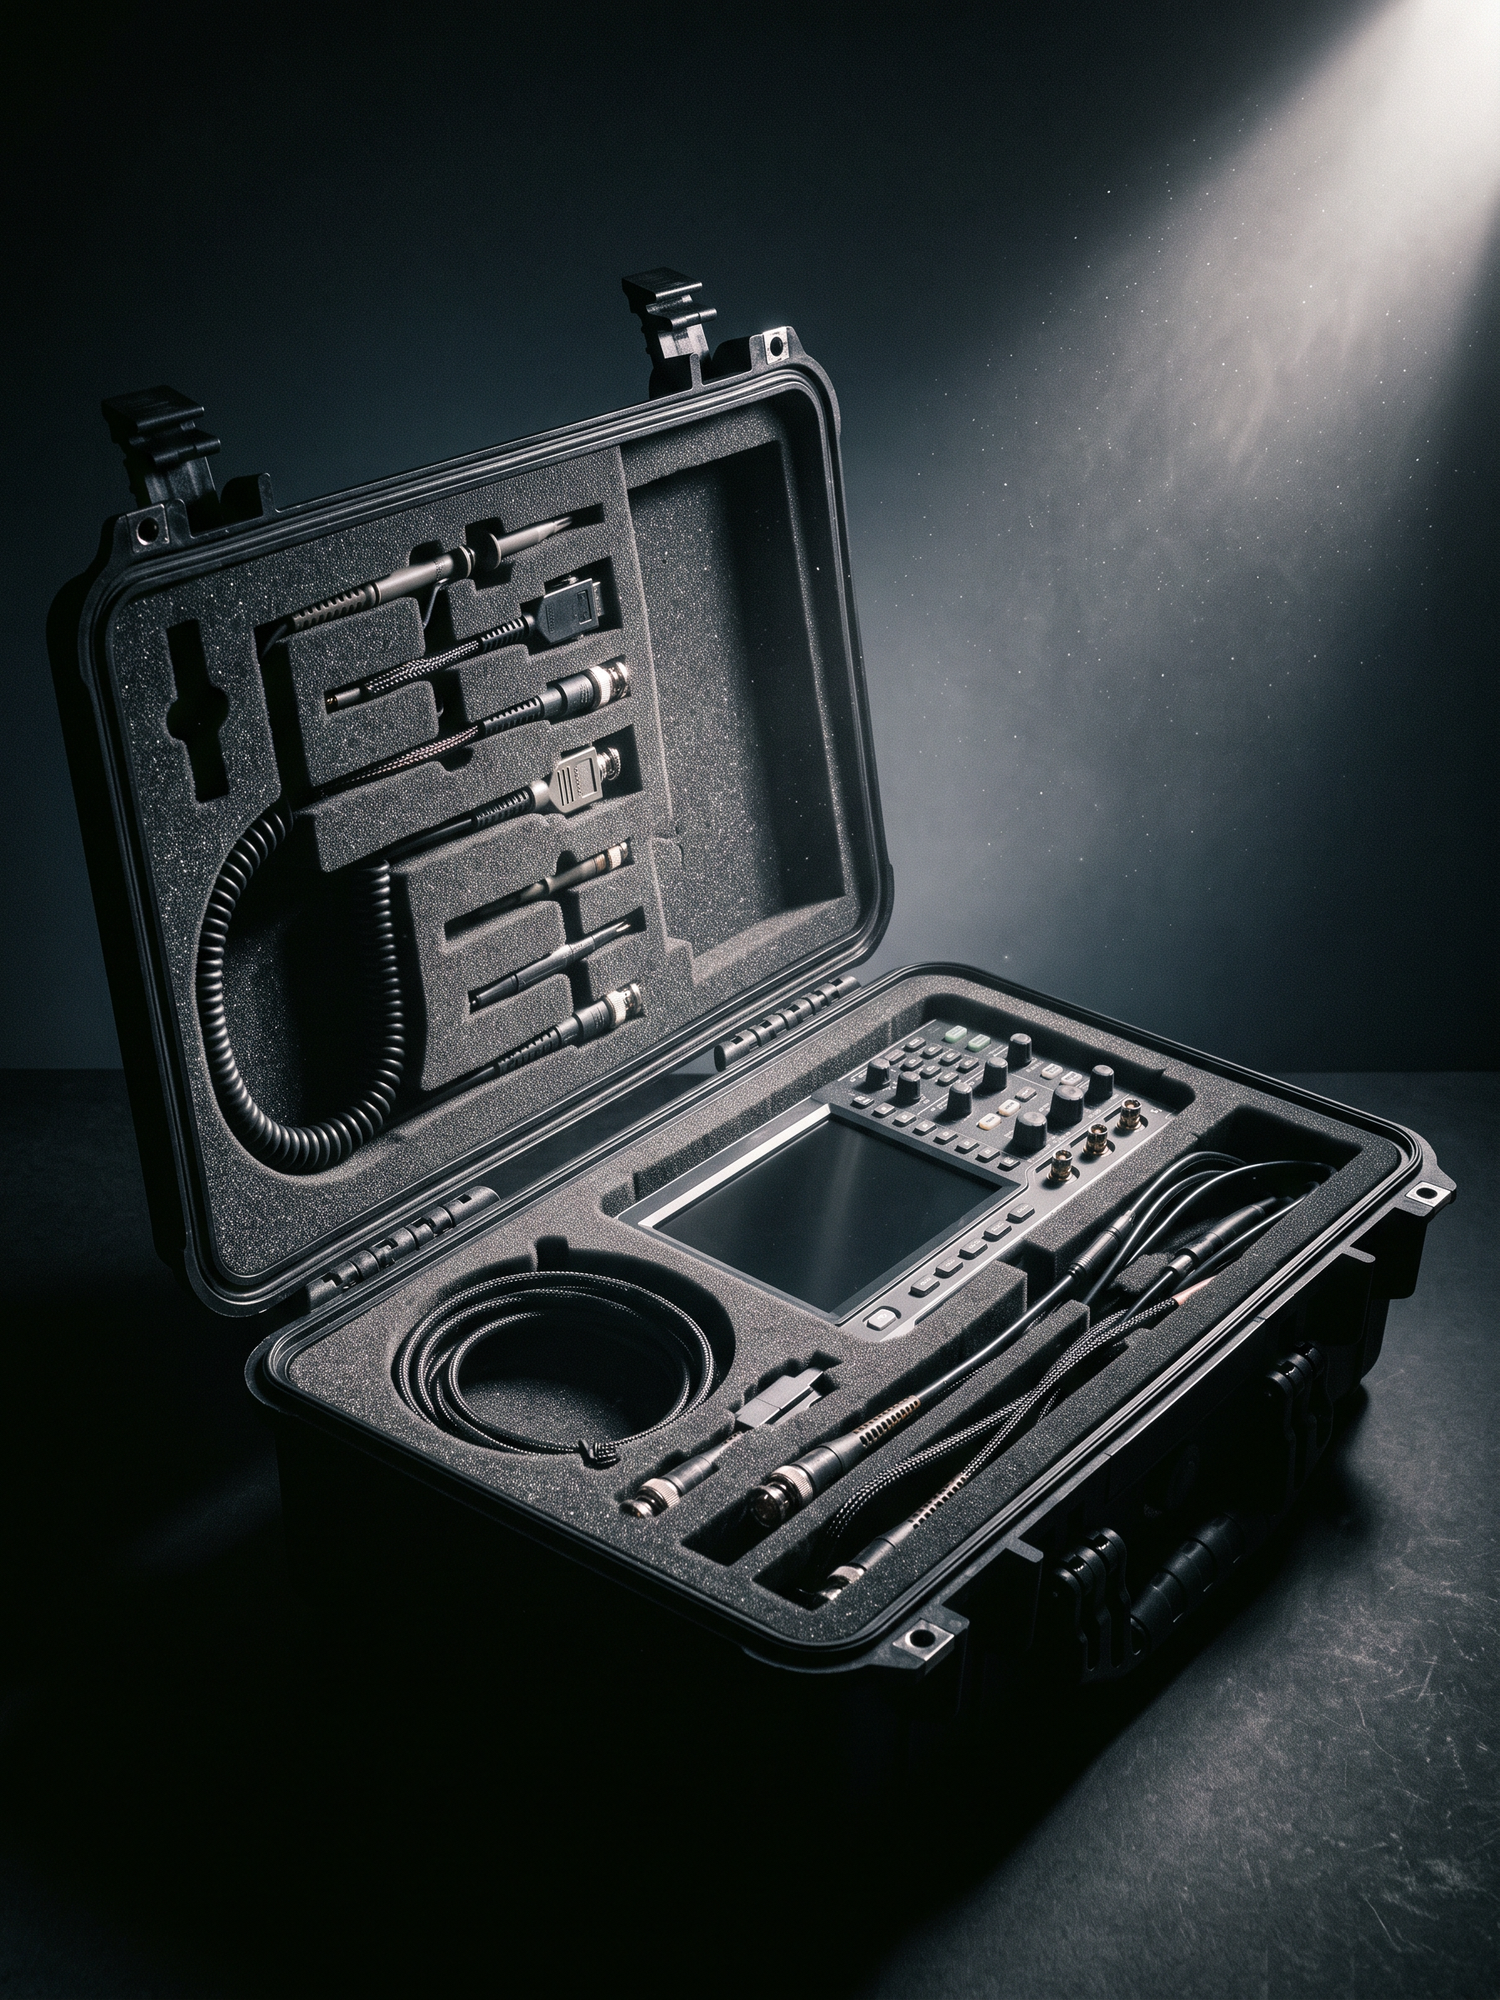
A pipeline detection equipment transport case is a professional-grade protective enclosure designed to safely store and transport precision pipeline detection instruments. Pipeline detection equipment encompasses a wide range of sophisticated devices — from CCTV inspection robots that travel inside pipelines to sonar detectors, ultrasonic detectors, and magnetic flux detectors used for external surveys. Each of these instruments contains precision optical, acoustic, and electronic components that demand rigorous protection.
KeXinMaterials pipeline detection equipment cases are engineered specifically for the pipeline detection industry. Every case is built to withstand the demanding conditions of field operations while providing the organization and accessibility that professionals need.
2. Core Protective Features
| Feature | Description |
|---|---|
| Waterproof | IP67-rated sealing prevents water ingress during fieldwork in wet conditions |
| Shockproof | High-density foam interior absorbs impact energy from drops and vibrations |
| Anti-static | ESD-safe lining protects sensitive electronic components from electrostatic discharge |
| Corrosion-resistant | Chemical-resistant shell materials withstand exposure to pipeline environments |
| Lightweight | Advanced composite materials minimize weight without compromising protection |
| Portable | Ergonomic handles and optional rolling wheels for easy field transport |
| Adjustable Dividers | Modular interior system organizes multiple accessories and tools |
| Custom Logo | Professional branding options for corporate and enterprise clients |
| Custom Colors | Choose colors that match your equipment fleet or corporate identity |
| Custom Foam | EVA foam or precision cut-out foam tailored to your specific detection equipment |
3. Applicable Equipment Types
- Pipeline CCTV inspection robot cases
- Pipeline sonar detector cases
- Pipeline ultrasonic detector cases
- Pipeline magnetic flux detector cases
These cases are designed for the safe storage and transport of precision pipeline detection instruments used in pipeline internal inspection and external detection operations.
4. Why Choose KeXinMaterials
Industry-Specific Expertise
KeXinMaterials specializes in protective case solutions for the pipeline detection industry. Our engineering team understands the unique demands of CCTV robots, sonar detectors, ultrasonic detectors, and magnetic flux detectors — and we build cases that meet those demands precisely.
Premium Materials & Construction
Every case features a high-strength polymer shell with IP67-rated sealing, precision-molded foam interiors, and corrosion-resistant hardware. The result is a transport case that performs reliably in the harshest pipeline environments.
Flexible Customization
From custom foam inserts matched to your specific equipment to branded exterior finishes, KeXinMaterials delivers cases built around your operational requirements — not a one-size-fits-all template.
Global B2B Service
With EXW and FOB delivery options from Shenzhen or Ningbo ports, KeXinMaterials serves pipeline detection companies, equipment distributors, and OEM partners worldwide.
5. FAQ
What is the MOQ for custom pipeline detection cases?
Our standard MOQ for custom-branded or custom-foam cases starts at 50 units. Please contact our sales team for a tailored quote based on your specifications.
What is the production lead time?
Standard cases ship within 7–15 working days. Custom configurations typically require 20–30 working days depending on complexity.
Can I get a sample before placing a bulk order?
Yes. Sample units are available for evaluation. Sample fees are credited upon confirmation of a bulk order.
What delivery terms do you offer?
We offer EXW and FOB terms from Shenzhen or Ningbo. Contact us for a freight quote to your destination.
Are the cases suitable for overseas field operations?
Absolutely. Our IP67-rated waterproof cases are designed for demanding field conditions and have been deployed by pipeline inspection teams operating in diverse environments globally.
Can you customize the foam insert for my specific detection equipment?
Yes. We offer precision laser-cut foam and custom EVA foam inserts tailored to the exact dimensions of your CCTV robot, sonar detector, ultrasonic detector, or magnetic flux detector.